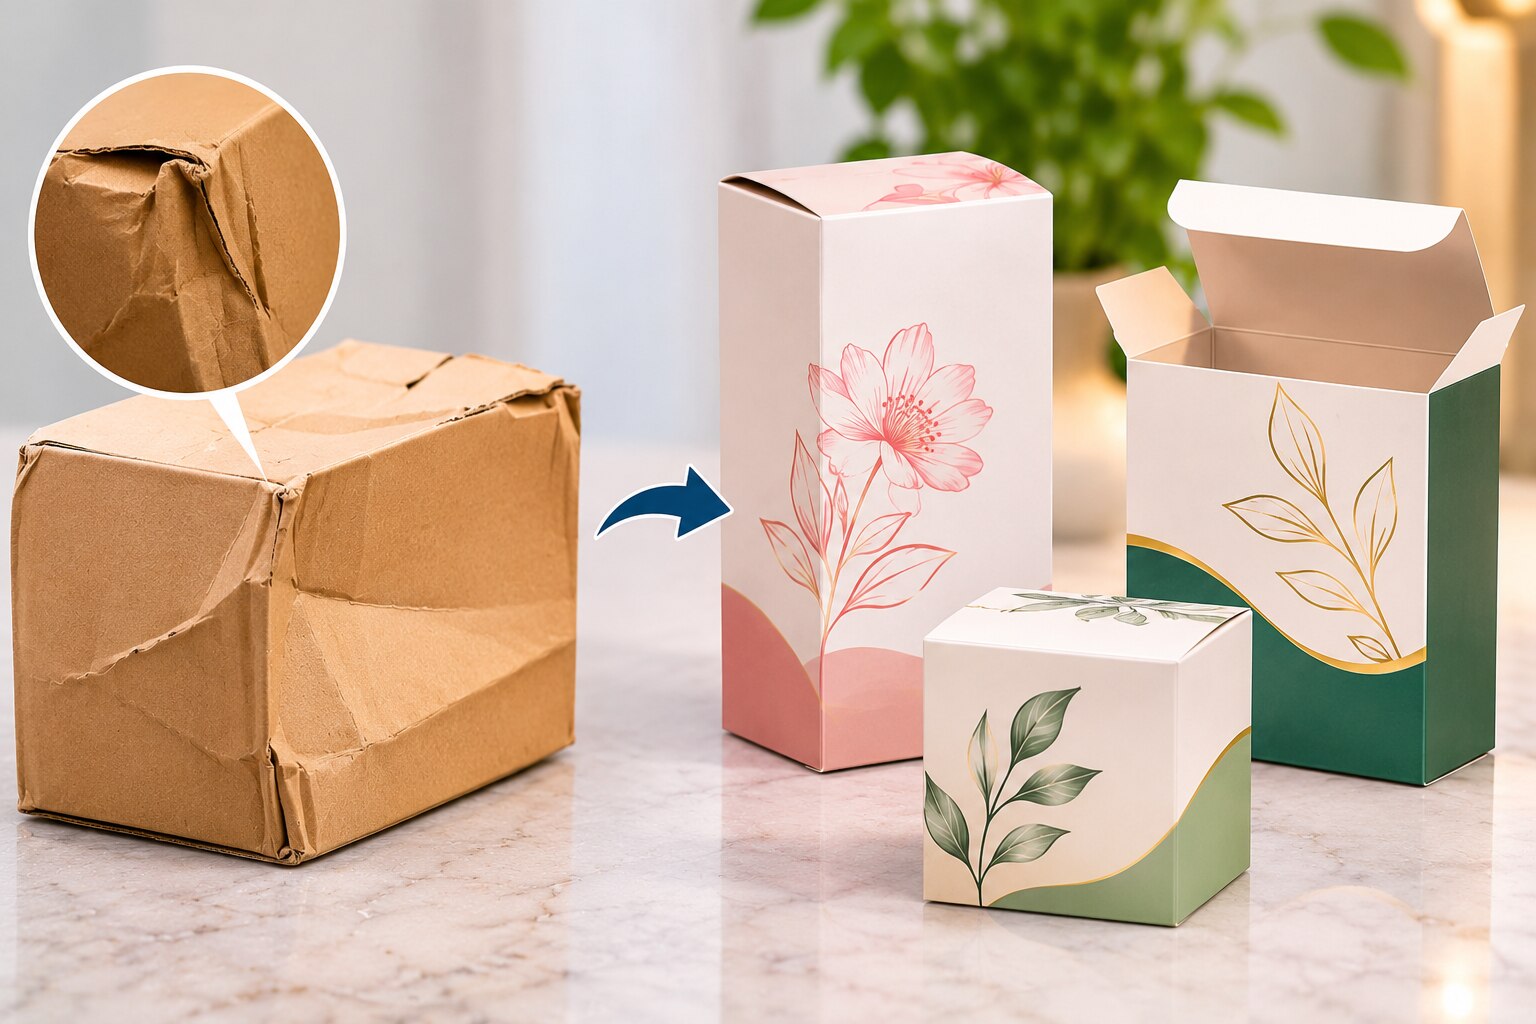
A crushed pack is not automatically proof that the carton board was too light. You need to identify whether the failure began in the panel, corner, crease, lock, insert, pallet, warehouse or transport route, then match the corrective action to that cause. By the end, you will have a practical supplier brief, investigation record and comparison method for selecting a stronger packaging solution.
Key takeaways
- Separate crushing, bulging, seam, score-line, and locking-tab failures before changing board.
- Record pack-line settings, batch numbers, pallet details, and delivery damage photographs.
- Request filled-pack compression, drop, vibration, and stacking evidence from your manufacturer.
- Use dividers, inserts, corrugated outers, or stronger systems when cartons cannot carry the load.
Identify the Failure Before Blaming the Board
A crushed corner, buckled panel, collapsed score line, open seam, torn locking tab, delamination, and product-induced bulging are different failures. Each points to a different cause, so a higher GSM board is not automatically the fix.
1. Inspect the damage on filled cartons, not only flat blanks. Record whether compression appears on the top panel, bottom panel, corners, glued seam, crease lines, or locking tabs. Check the product too: a bottle shoulder, tight insert, uneven fill, or cap pressure can push outward and create bulging that looks like weak board.
2. Compare empty and filled cartons after erection. Oversized internal clearance allows the pack to shift and transfers impact to corners; a poorly designed die-cut, shallow or over-compressed crease, wrong grain direction, weak locking structure, or excessive panel width can trigger buckling and collapse.
3. Check the distribution conditions before blaming converting. Heat, monsoon humidity, long warehouse dwell time, excessive stack height, case compression, pallet overhang, void space, rough handling, and transport vibration can weaken paperboard or crush cartons inside a secondary case.
4. Record the SKU, carton dimensions, board grade, grammage, caliper, batch number, packing date, pallet pattern, stack height, route, storage humidity, and photographs. This separates crushed mono cartons in Jaipur from a filling-line, pallet, or logistics problem and makes recurring carton packaging failure for brands traceable to a specific lot.
Build a Traceable Damage Record From Pack Line to Delivery
Photograph each failed pack before opening it, then match it to a carton lot, filling shift, pallet and delivery record. A product packaging damage manufacturer should provide lot traceability for board mill or grade, production date, die and crease settings, printing and coating process, packing date and retained samples.
Without that chain, a recurring failure remains a guess.
Collect these records for every incident:
- SKU, carton dimensions, board grade and caliper, batch number, packing date and filling line
- Damage location and form: panel crush, corner collapse, buckling, delamination, seam failure, torn locking tab or product bulge
- Pallet pattern, case dimensions, void space, stack height, pallet overhang, warehouse dwell time and storage humidity
- Transport route, carrier, delivery date, photographs of pallet condition and outer-case compression
Run a controlled comparison with the same product, filling line, case configuration, pallet pattern and distribution route. Change only the carton specification; changing several variables can hide the cause. Inspect empty cartons, filled cartons at pack-out, cases after storage and units at delivery.
A defect visible before case packing points to board or converting. Damage appearing during filling points to internal clearance, inserts or machine pressure; damage first seen after storage or transit points to humidity, stacking or handling.
For shipment failures, test complete filled transport packages under ISO 12048 and set an acceptance criterion tied to the route. Retain failed and accepted samples for comparison.
Specify the Structure That Resists Crushing
A crush-resistant filled mono carton starts with a matched structure, not a higher GSM number. Specify the paperboard grade, caliper range, bending stiffness, moisture limit and grain direction for the actual carton dimensions and product weight. Oversized internal clearance lets the product move and buckle panels; excessive panel width creates the same problem.
| Feature | Specify | Failure prevented |
|---|---|---|
| Board construction | Board grade, caliper range, bending stiffness and grain direction | Panel crushing and corner collapse |
| Creases | Score width and depth trialled for the board, grain and folding equipment | Buckling from shallow scores; hinge fracture or tearing from deep scores |
| Die-cut | Accurate panel geometry, cut-line and crease tolerances, with clean corners | Misalignment, weak corners and uneven erection |
| Locking system | Adequate tab length, slot clearance and glued-seam width | Open seams, torn tabs and lock release |
| Panel design | Panel widths matched to the filled product, with minimal unused clearance | Product-induced bulging and unsupported faces |
| Finishing | Coating and varnish compatible with folding; no cracking over scores; controlled moisture pickup | Brittle folds, delamination and humidity-related softening |
A strong mono carton supplier in Jaipur should test the filled carton, not judge strength from GSM alone. Confirm column-stacked and interlocked pallet trials separately: interlocking can reduce vertical compression, while pallet overhang bends exposed edges. Define a compression or distribution-test pass criterion, stack height, pallet limits and storage humidity in the specification.
Demand Filled-Pack Evidence From the Manufacturer
Approve a supplier only after it proves that the filled carton survives your actual product, filling line, case pack, pallet pattern and delivery route—not merely an empty-box compression test.
1. Request three sample sets: the current failed carton, the proposed revision, and a control carton that has passed distribution. Require each sample to be filled with the real product, including the actual bottle shoulders, cap pressure, insert and product clearance.
2. Ask for a written specification covering board grade, grammage, caliper, grain direction, panel dimensions, crease depth, die-cut layout, locking-tab dimensions, glued-seam width, coating and internal clearance. Record tolerances for carton length, width, height, caliper, crease position and squareness; reject vague terms such as “premium board.”
3. Require lot traceability for board mill or grade, production date, die and crease settings, printing and coating process, packing date and retained samples. A product packaging damage manufacturer that cannot trace these details cannot isolate a material, converting or filling-line fault.
4. Run a controlled comparison with one variable changed at a time. Measure filled-carton top-load or compression strength, seam and lock integrity, dimensional fit, vibration, drop and pallet compression performance, then record the failure location and load at failure.
5. Set pass/fail limits before testing, including permitted crushed corners, panel buckling, open seams, torn tabs and permanent deformation. Test column-stacked and interlocked pallets, with the actual case dimensions, void space, stack height, overhang, humidity exposure and warehouse dwell time.
Riya Creation should be evaluated on this evidence package, not a higher GSM quote alone. The best mono carton manufacturer in Jaipur for crushed product packs will explain which failure mode the revision fixes and show repeatable results across retained production samples.
Related product
 | Mono Carton Leading mono carton box manufacturer offering custom printed packaging, duplex carton boxes, pharmaceutical, cosmetic, food, FMCG, retail, and... View product → |
Know When a Mono Carton Needs a Stronger Packaging System
Keep the mono carton when its panels and seams remain intact and damage comes from handling or movement inside the pack. Add an insert when the product shifts or its shoulders press the top; add a stronger secondary pack when the individual cartons pass inspection but the shipping case collapses.
Replace the system with a corrugated shipper when filled units must carry distribution loads beyond the carton’s design, or when damage continues after correcting case fit and pallet loading. Check void space, case compression, pallet overhang, stack height, and warehouse dwell time before blaming the printed carton.
Column-stacked cases usually preserve compression better than interlocked patterns.
Choose a rigid box when presentation and impact protection justify higher material, assembly, and freight costs. It will not fix humid storage or a weak pallet pattern.
Do not approve a higher-GSM board without a filled-pack trial that reproduces the actual product, insert, closure, case, and pallet. The corrective choice should follow the failure mode:
- Retain and reinforce the mono carton for isolated corner impacts or minor panel buckling.
- Add an insert for product movement or pressure from bottle shoulders and caps.
- Add a stronger secondary pack for case compression and transport vibration.
- Replace the system after repeated seam failure, torn locking tabs, or product damage despite added protection.
Record the result by SKU and batch. That evidence separates carton packaging failure for brands from logistics damage, including crushed mono cartons in Jaipur distribution routes.
Frequently asked questions
How do you identify the cause of a crushed mono carton?
Match the visible failure to its location and pattern: corners, panels, score lines, seams, tabs, layers, or product contact points indicate different causes.
What should a damage record include for crushed product packs?
Record the carton batch, product batch, pack-line settings, pallet configuration, transport conditions, delivery photographs, and the percentage of damaged packs.
What carton specifications help resist crushing?
Specify board grade and thickness, carton dimensions, grain direction, score-line design, locking structure, seam construction, and the required filled-pack tests.
What evidence should a mono carton manufacturer provide?
Ask for filled-pack compression, drop, vibration, stacking, seam, and storage-condition test results using your actual product and carton design.
When does a mono carton need a stronger packaging system?
Add inserts, dividers, a corrugated outer, protective wrap, or a redesigned pack when the product carries load, shifts inside, or exceeds the carton’s compression capacity.
Keywords